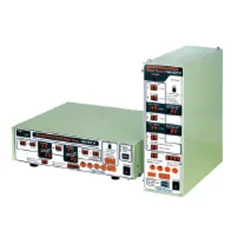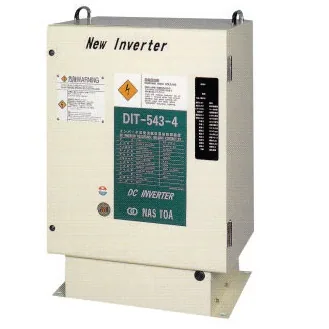

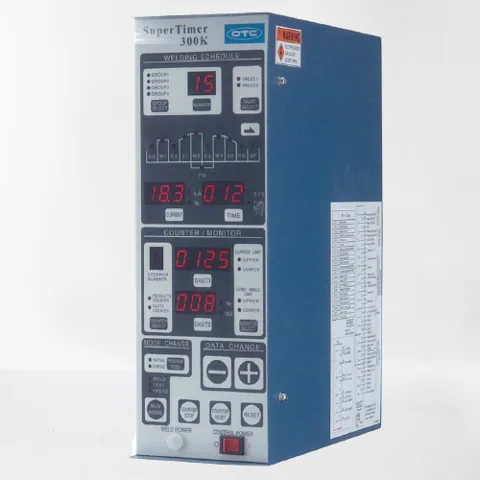
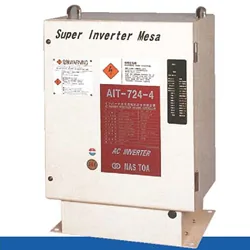
AC Inverter Controller AIT
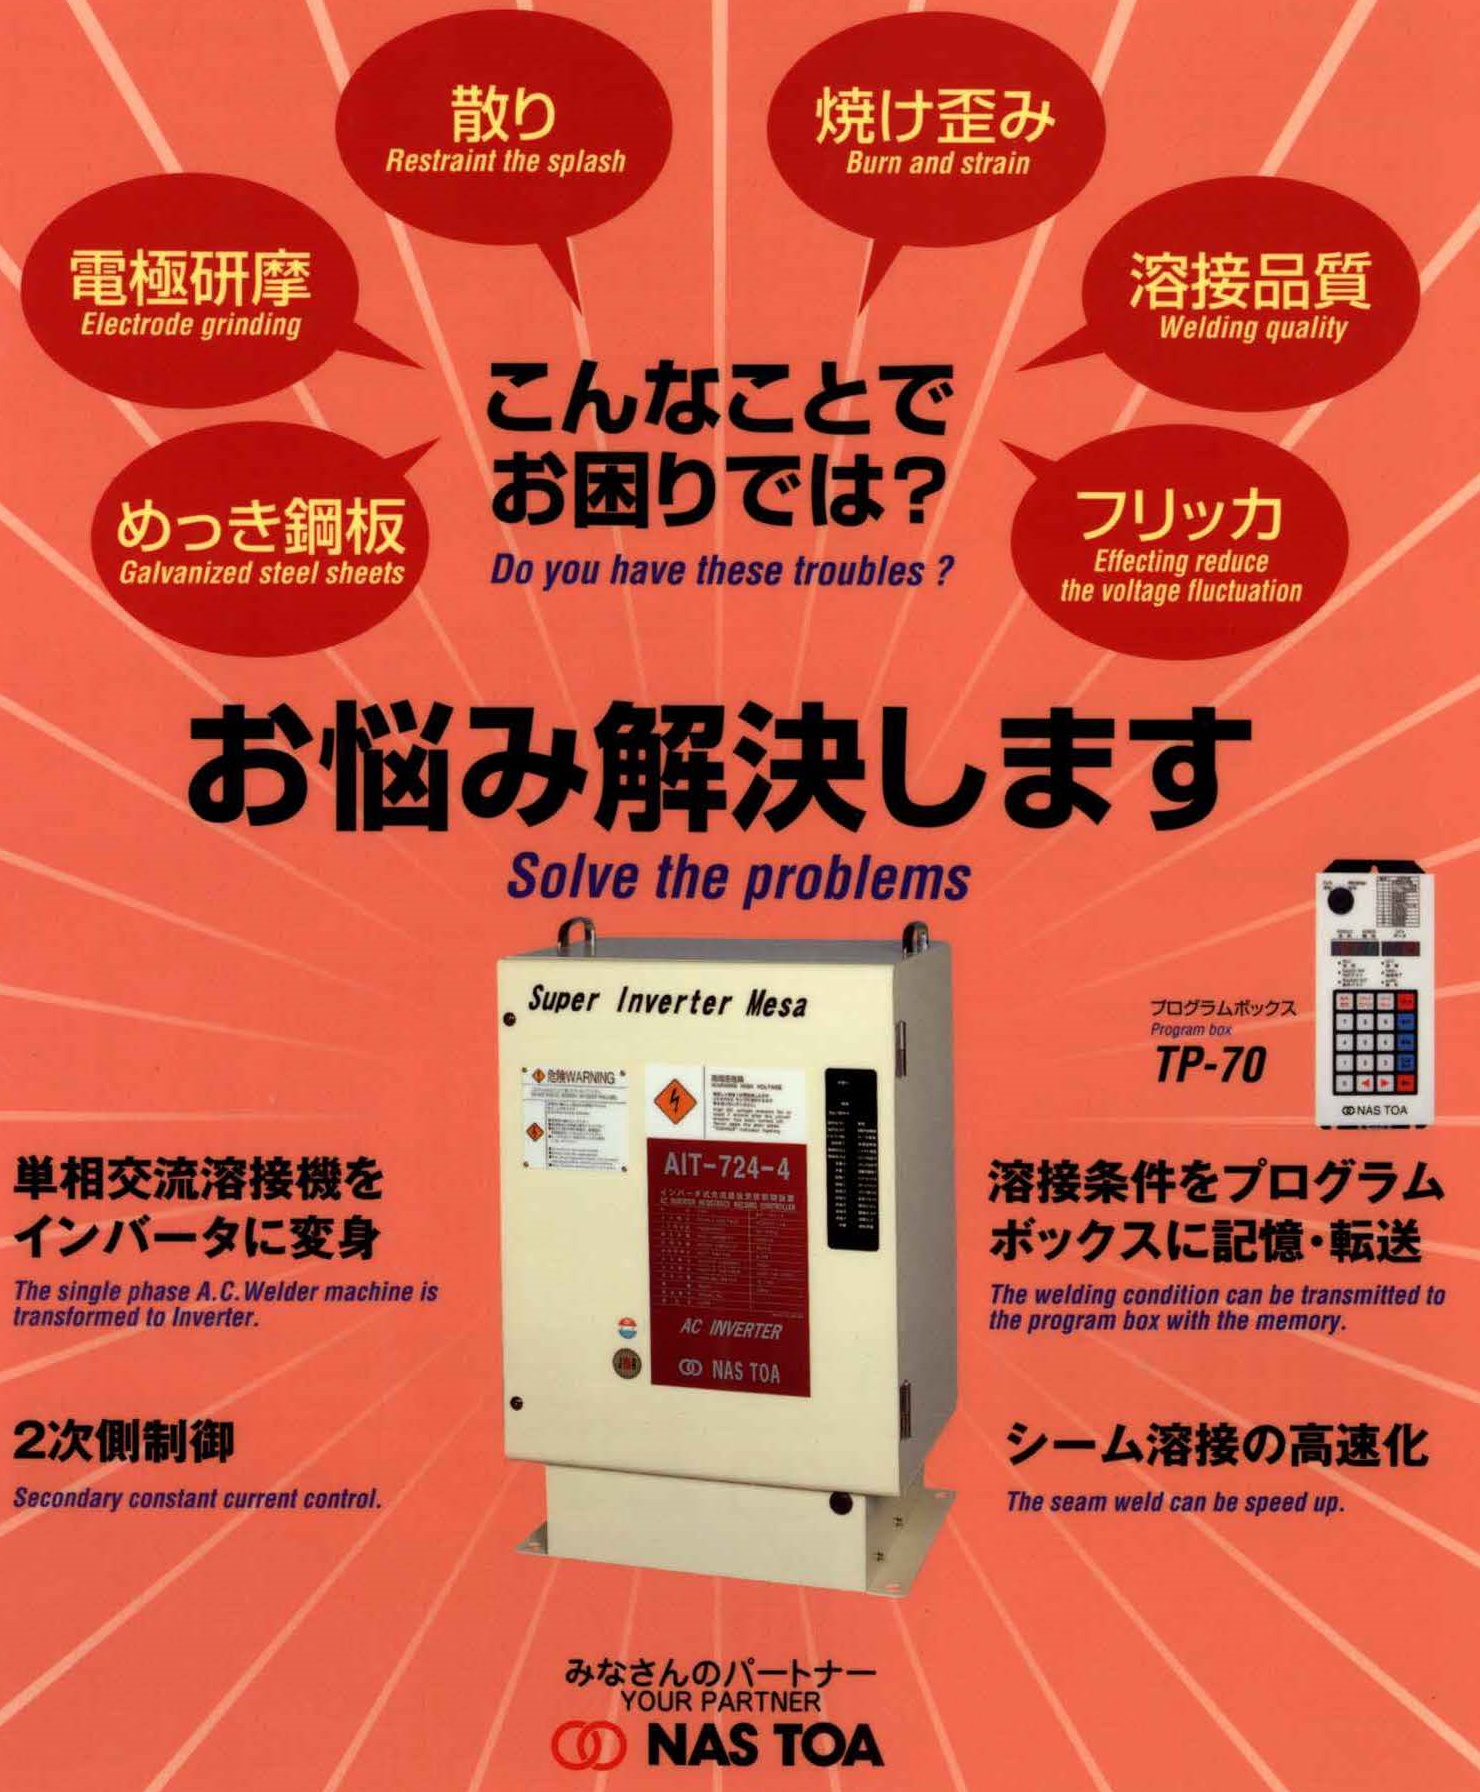
Do you have these troubles? Galvanized steel sheets Electrode grinding Restraint the splash Burn and strain Welding quality. Effecting reducing the voltage fluctuation. Solve the problems Secondary constant current…
In your quote View quote
Ask on WhatsAppNo prices online: our sales team replies with a quotation, lead time and advice for your application.
- Category
- Weld Controller
- Datasheets
- 1 PDF
Details
Do you have these troubles?
- Galvanized steel sheets
- Electrode grinding
- Restraint the splash
- Burn and strain
- Welding quality.
- Effecting reducing the voltage fluctuation.
Solve the problems
- Secondary constant current control
- The single phase A.C. Welder machine is transformed
- The Welding condition can be transmitted to the program box with the memory
- The seam weld can be speed up.
- Current not consistency
- Part rejection very high
- Worry of welding quality
- High power input consumption
- Long weld time
- Change new super inverter mesa AIT series
- No need controller
- No need thyristor
- Old machine parts service
- Working Smooth
- Good output quality
- Constant current output
- Low power input (40% lower compare AC machine)
- Shorter weld time
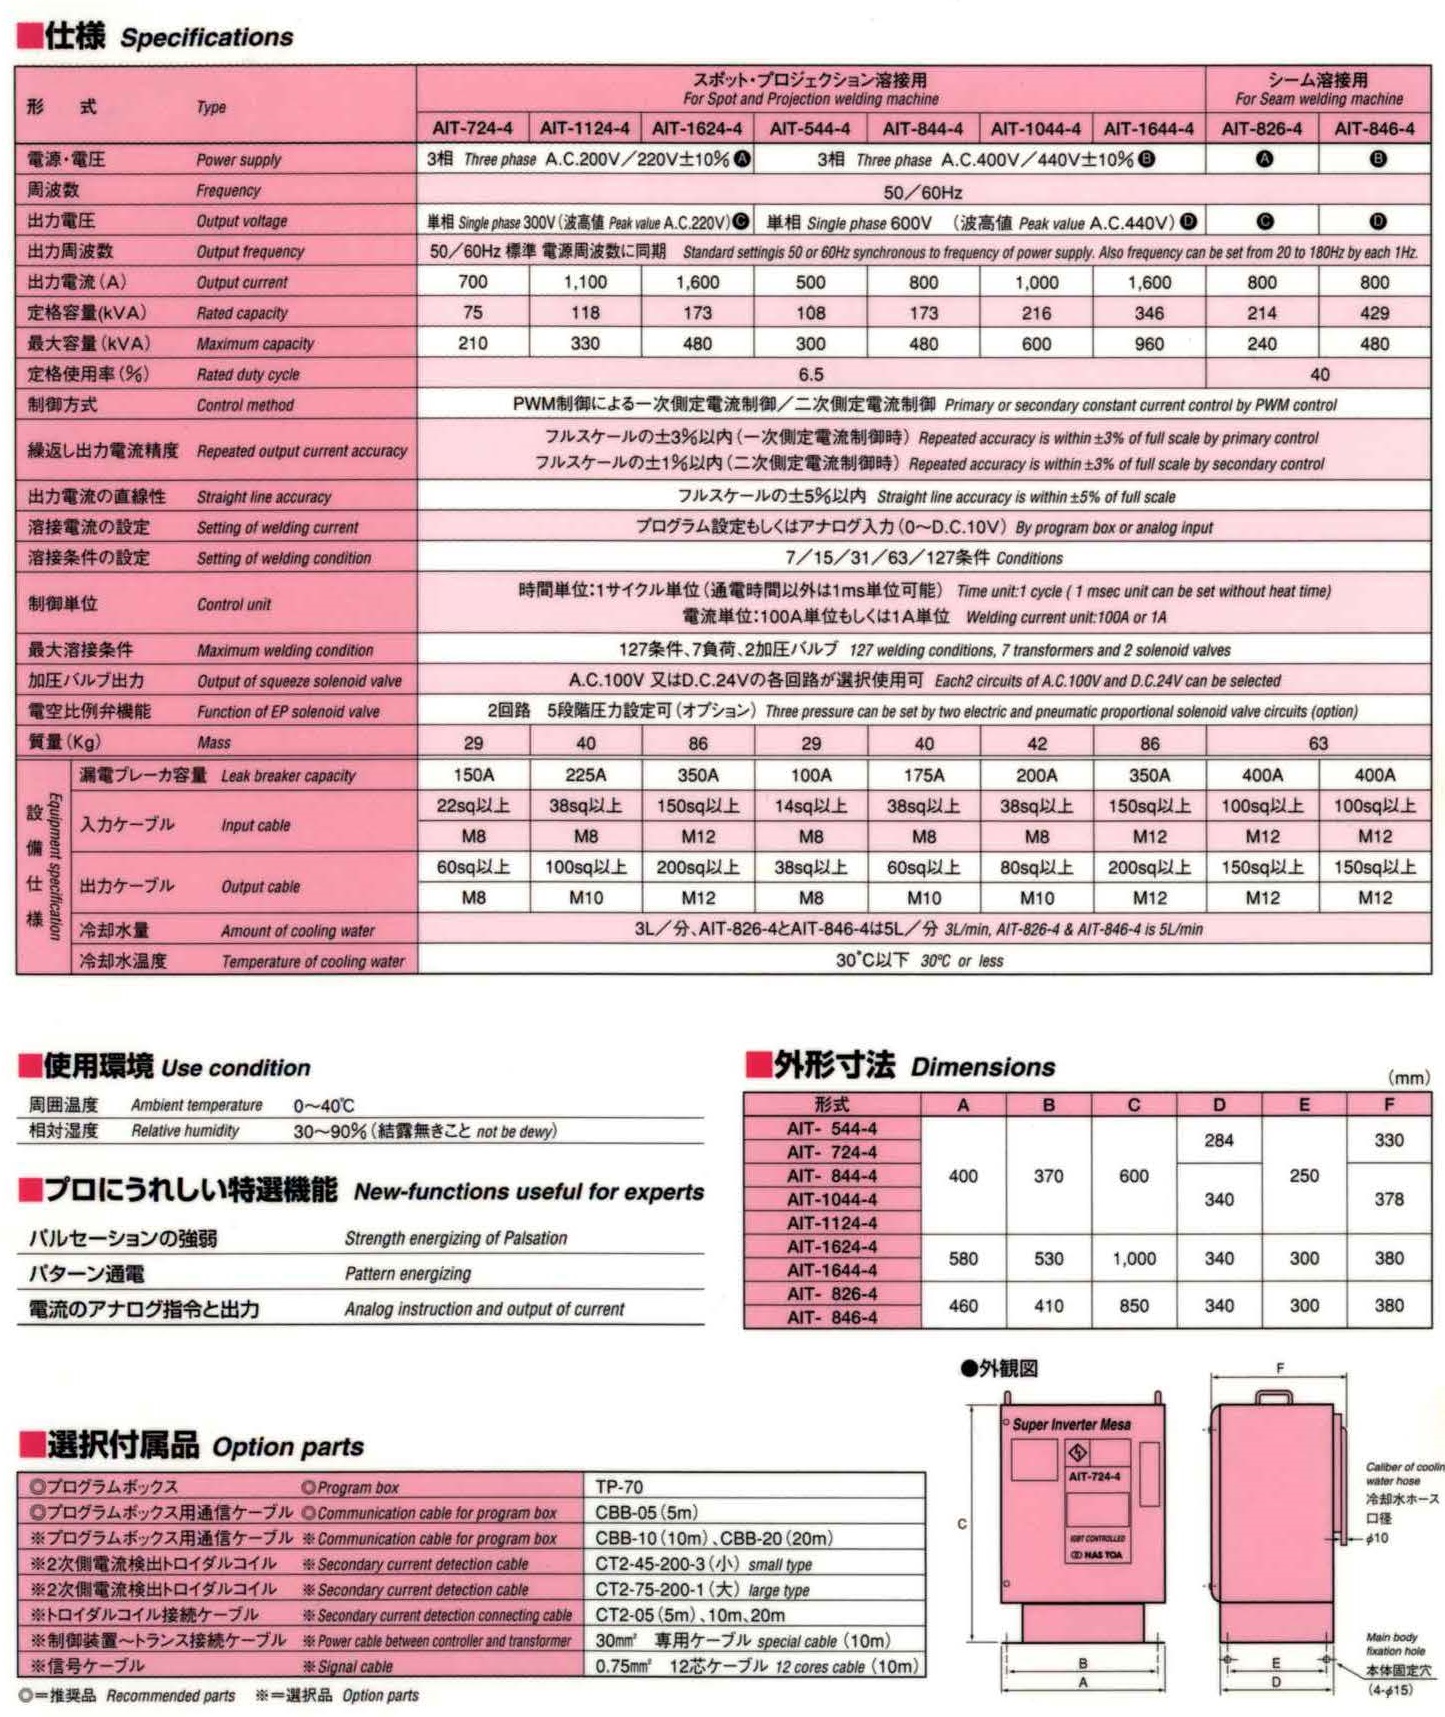
Specification
| Type | For Spot and Projection welding machine | For Seam welding machine | |||||||
| AIT-724-4 AIT-1124-4 AIT-1624-4 | AIT-544-4 AIT-844-4 AIT-1044-4 AIT-1644-4 | AIT-826-4 | AIT846-4 | ||||||
| Power Supply | Three phase A.C.200V/220V±10% | Three phase A.C.400V/440V±10% | |||||||
| Frequency | 50/60Hz | ||||||||
| Output voltage | Single phase 300V (Peak value A.C.220V) | Single phase 600V (Peak value A.C.440V) | |||||||
| Output frequency | Standard settings 50 or 60 Hz synchronous to frequency of power supply. Also frequency can be set from 20 to 180Hz by each 1Hz | ||||||||
| Output current | 700 | 1100 | 1600 | 500 | 800 | 1000 | 1600 | 800 | 800 |
| Rated capacity | 75 | 118 | 173 | 108 | 173 | 216 | 346 | 214 | 429 |
| Maximum capacity | 210 | 330 | 480 | 300 | 480 | 600 | 960 | 240 | 480 |
| Rated duty cycle | 6.5 | 40 | |||||||
| Control method | Primary or secondary constant current by PWM control | ||||||||
| Repeated output currency accuracy | Repeated accuracy is within ±3% of scale by primary control
Repeated accuracy is within ±3% of scale by secondary control |
||||||||
| Straight line accuracy | Straight line accuracy is within ±5% of full scale | ||||||||
| Setting of welding current | By program box or analog input | ||||||||
| Setting of welding condition | 7/15/31/63/127 Conditions | ||||||||
| Control unit | Time unit : 1 cycle (1msec unit can be set without heat time)
Weelding current unit : 100A or 1A |
||||||||
| Maximum welding condition | 127 welding conditions, 7 transformers and 2 solenoid valves | ||||||||
| Output squeeze solenoid valve | Each circuits of A.C.100V and D.C.24V can be selected | ||||||||
| Function of EP solenoid valve | Three pressure can be set by two electric and pneumatic proportional solenoid valve circuits (option) | ||||||||
| Mass | 29 | 40 | 86 | 29 | 40 | 42 | 86 | 63 | |
| Lead beaker capacity | 150A | 225A | 350A | 100A | 175A | 200A | 350A | 400A | 400A |
| Input cable | 22sq
M8 |
38sq
M8 |
150sq
M12 |
14sq
M8 |
38sq
M8 |
38sq
M8 |
150sq
M12 |
100sq
M12 |
100sq
M12 |
| Output cable | 60sq
M8 |
100sq
M10 |
200sq
M12 |
38sq
M8 |
60sq
M10 |
80sq
M10 |
200sq
M12 |
150sq
M12 |
150sq
M12 |
| Amount of cooling water | 3L/min, AIT-825-4 & AIT-846-4 is 5L/min | ||||||||
| Temperature of cooling water | 30ºC or less | ||||||||
PDF Download
ac inverter